Repeatable OD, ID, grooves and simple thread features are good production candidates.
REPEAT-PRODUCTION TURNING
Automatic Lathe Machining for Repeat-Volume Turned Parts
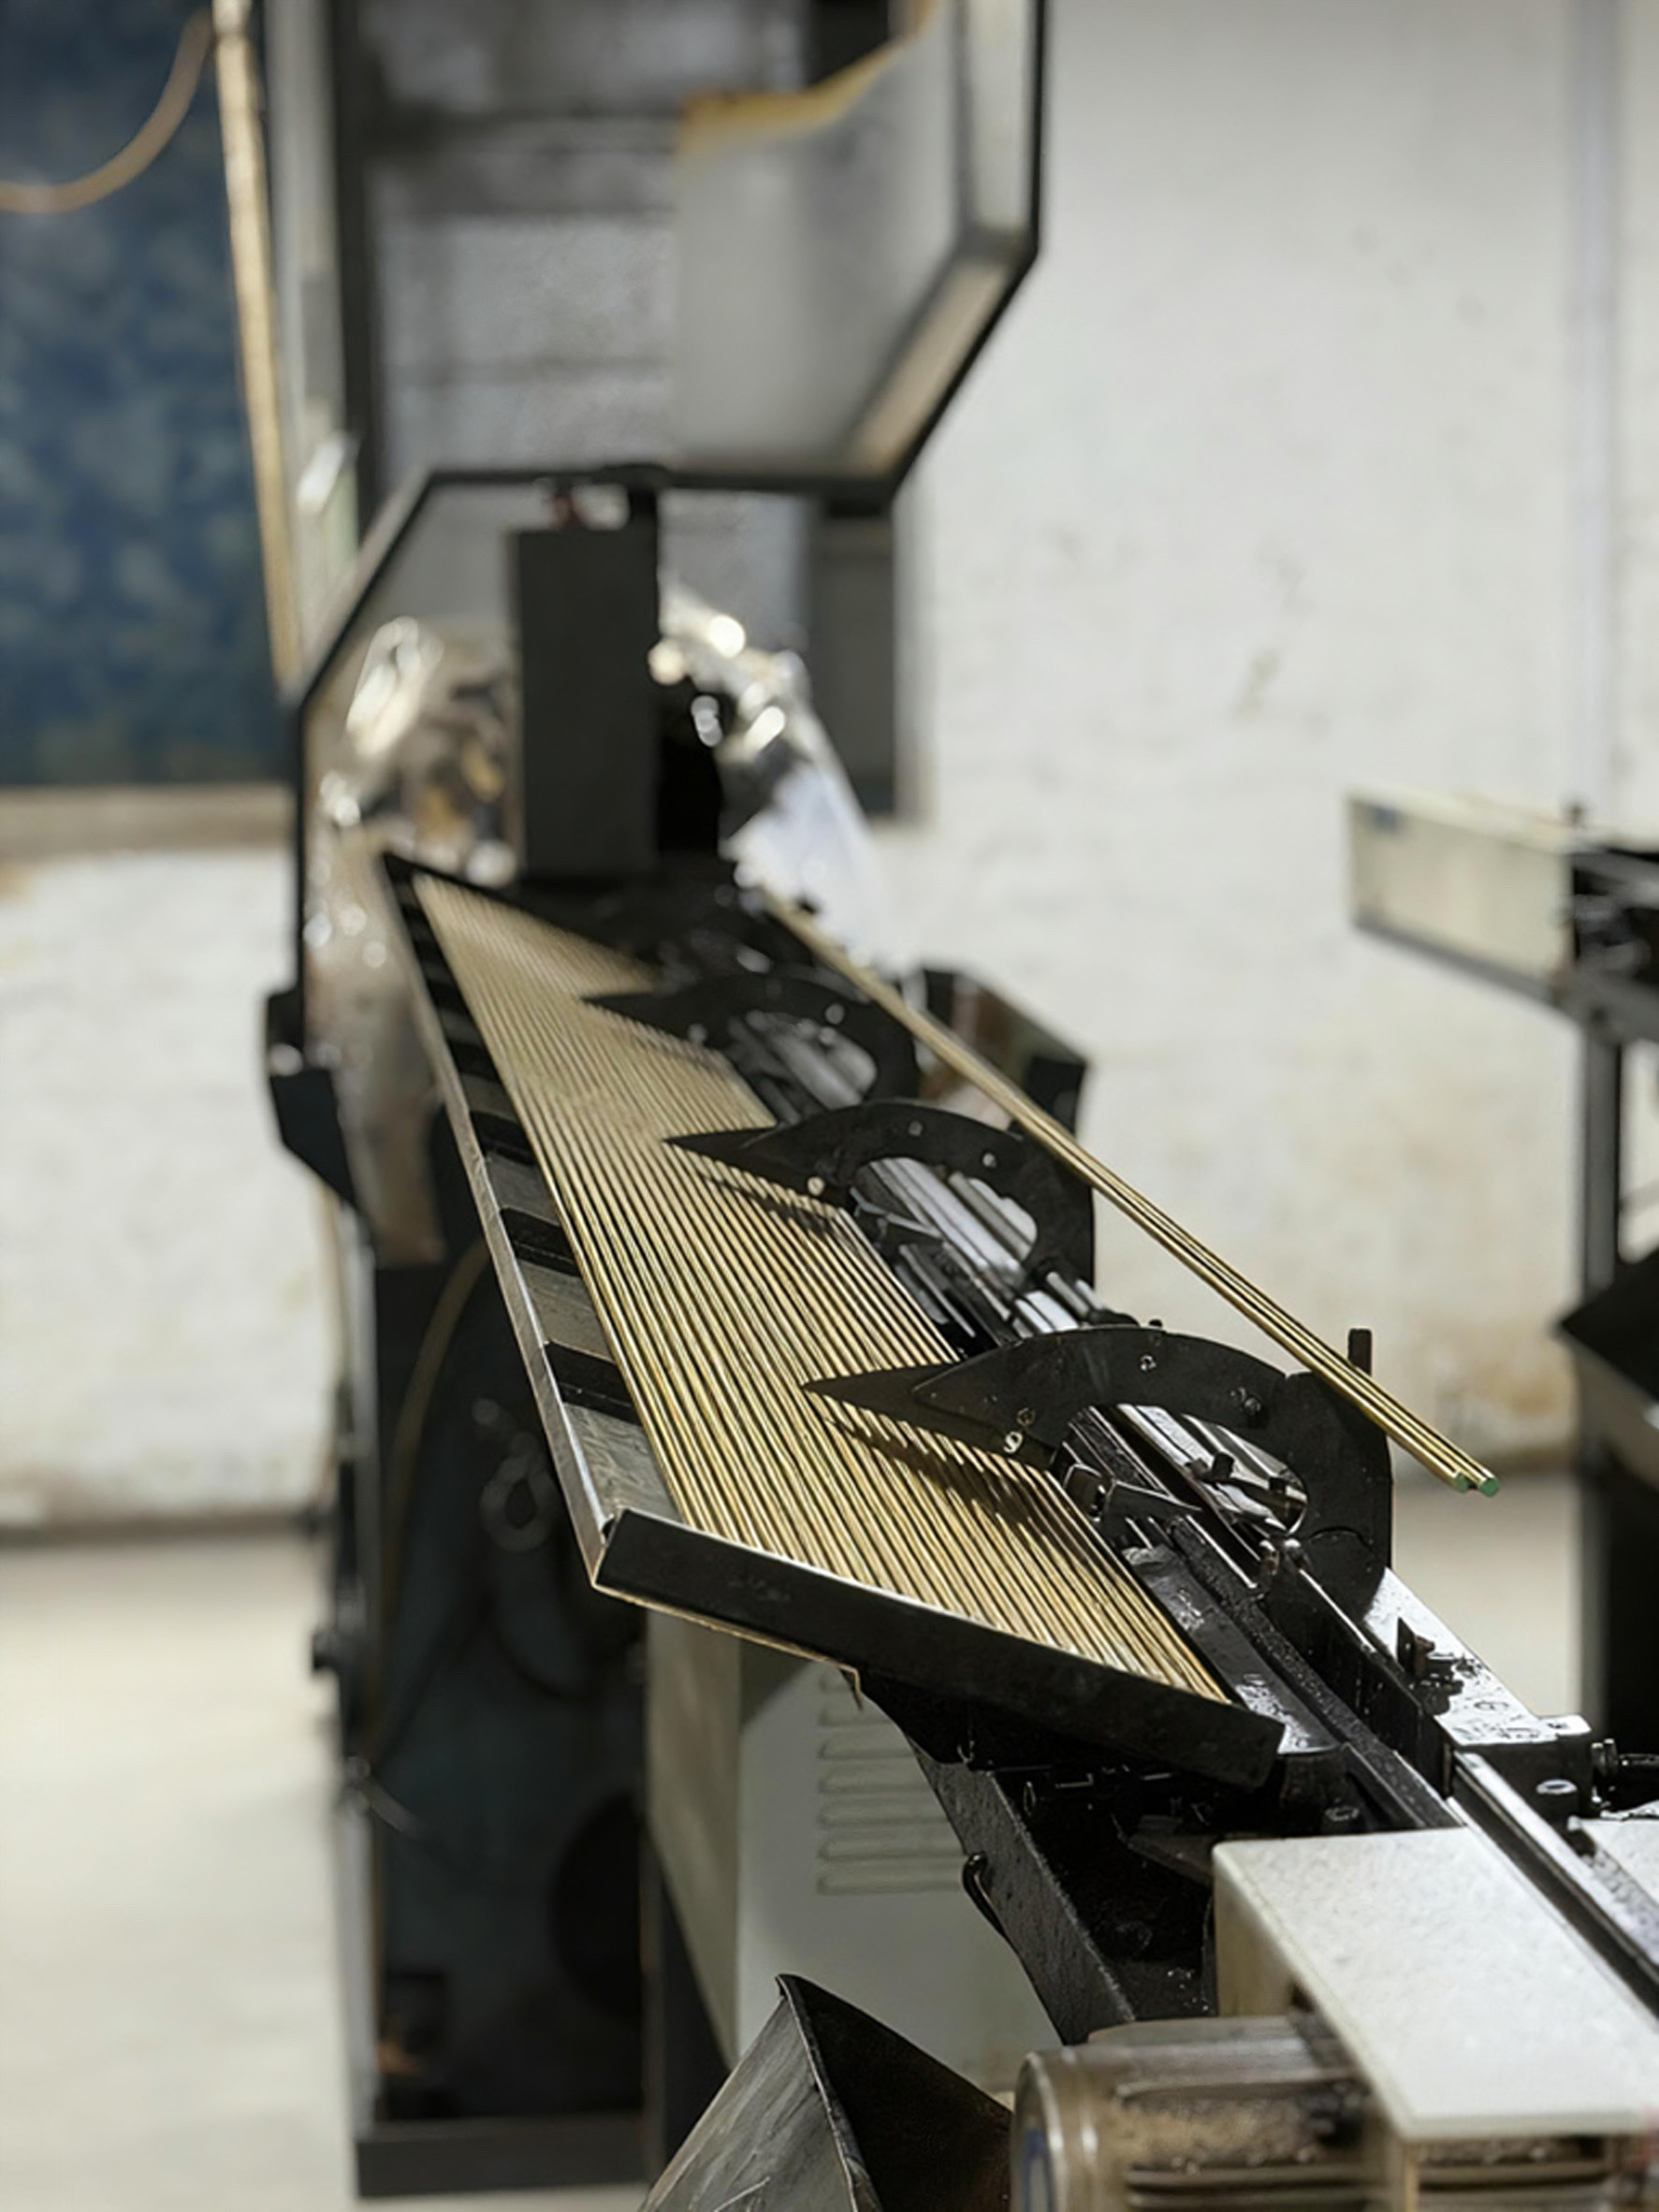
Automatic lathe machining supports stable repeat-volume turned parts where geometry is proven and production efficiency matters. It complements FREEFLY CNC’s Swiss turning and CNC turning routes.
Part geometry, expected quantity, material behavior and secondary features determine whether automatic-lathe production is the right route.
repeat rhythm / bar to batch
~±0.01 mmTypical tolerance on suitable features
~7 DaysTypical sample route, project-dependent
500+ pcsProduction strength, samples supported
ISO 9001Quality management system
/ Production Fit
When repeat demand shapes the route
Automatic-lathe routing is most useful when the part geometry is stable and expected demand supports repeat production.
500+ pcs can align with production planning, but it is not a blanket minimum.
Bar stock condition and machinability affect consistency.
Many cross holes, flats or slots may require a combined route.
/ Route Comparison
Choose the turning route by part requirement
Different turning processes serve different geometry, support and production needs.
Strong fit for small, slender, bar-fed precision components up to approx. Ø38 mm where suitable.
Flexible route for rotational components, prototypes and varied geometry.
Useful for stable repeat-volume turned parts where setup economics support it.
Adds holes, flats, deburr, finish or inspection after the base turning route.
/ Part Families
Repeat parts commonly reviewed
These examples help buyers decide whether quantity and geometry should be discussed together.
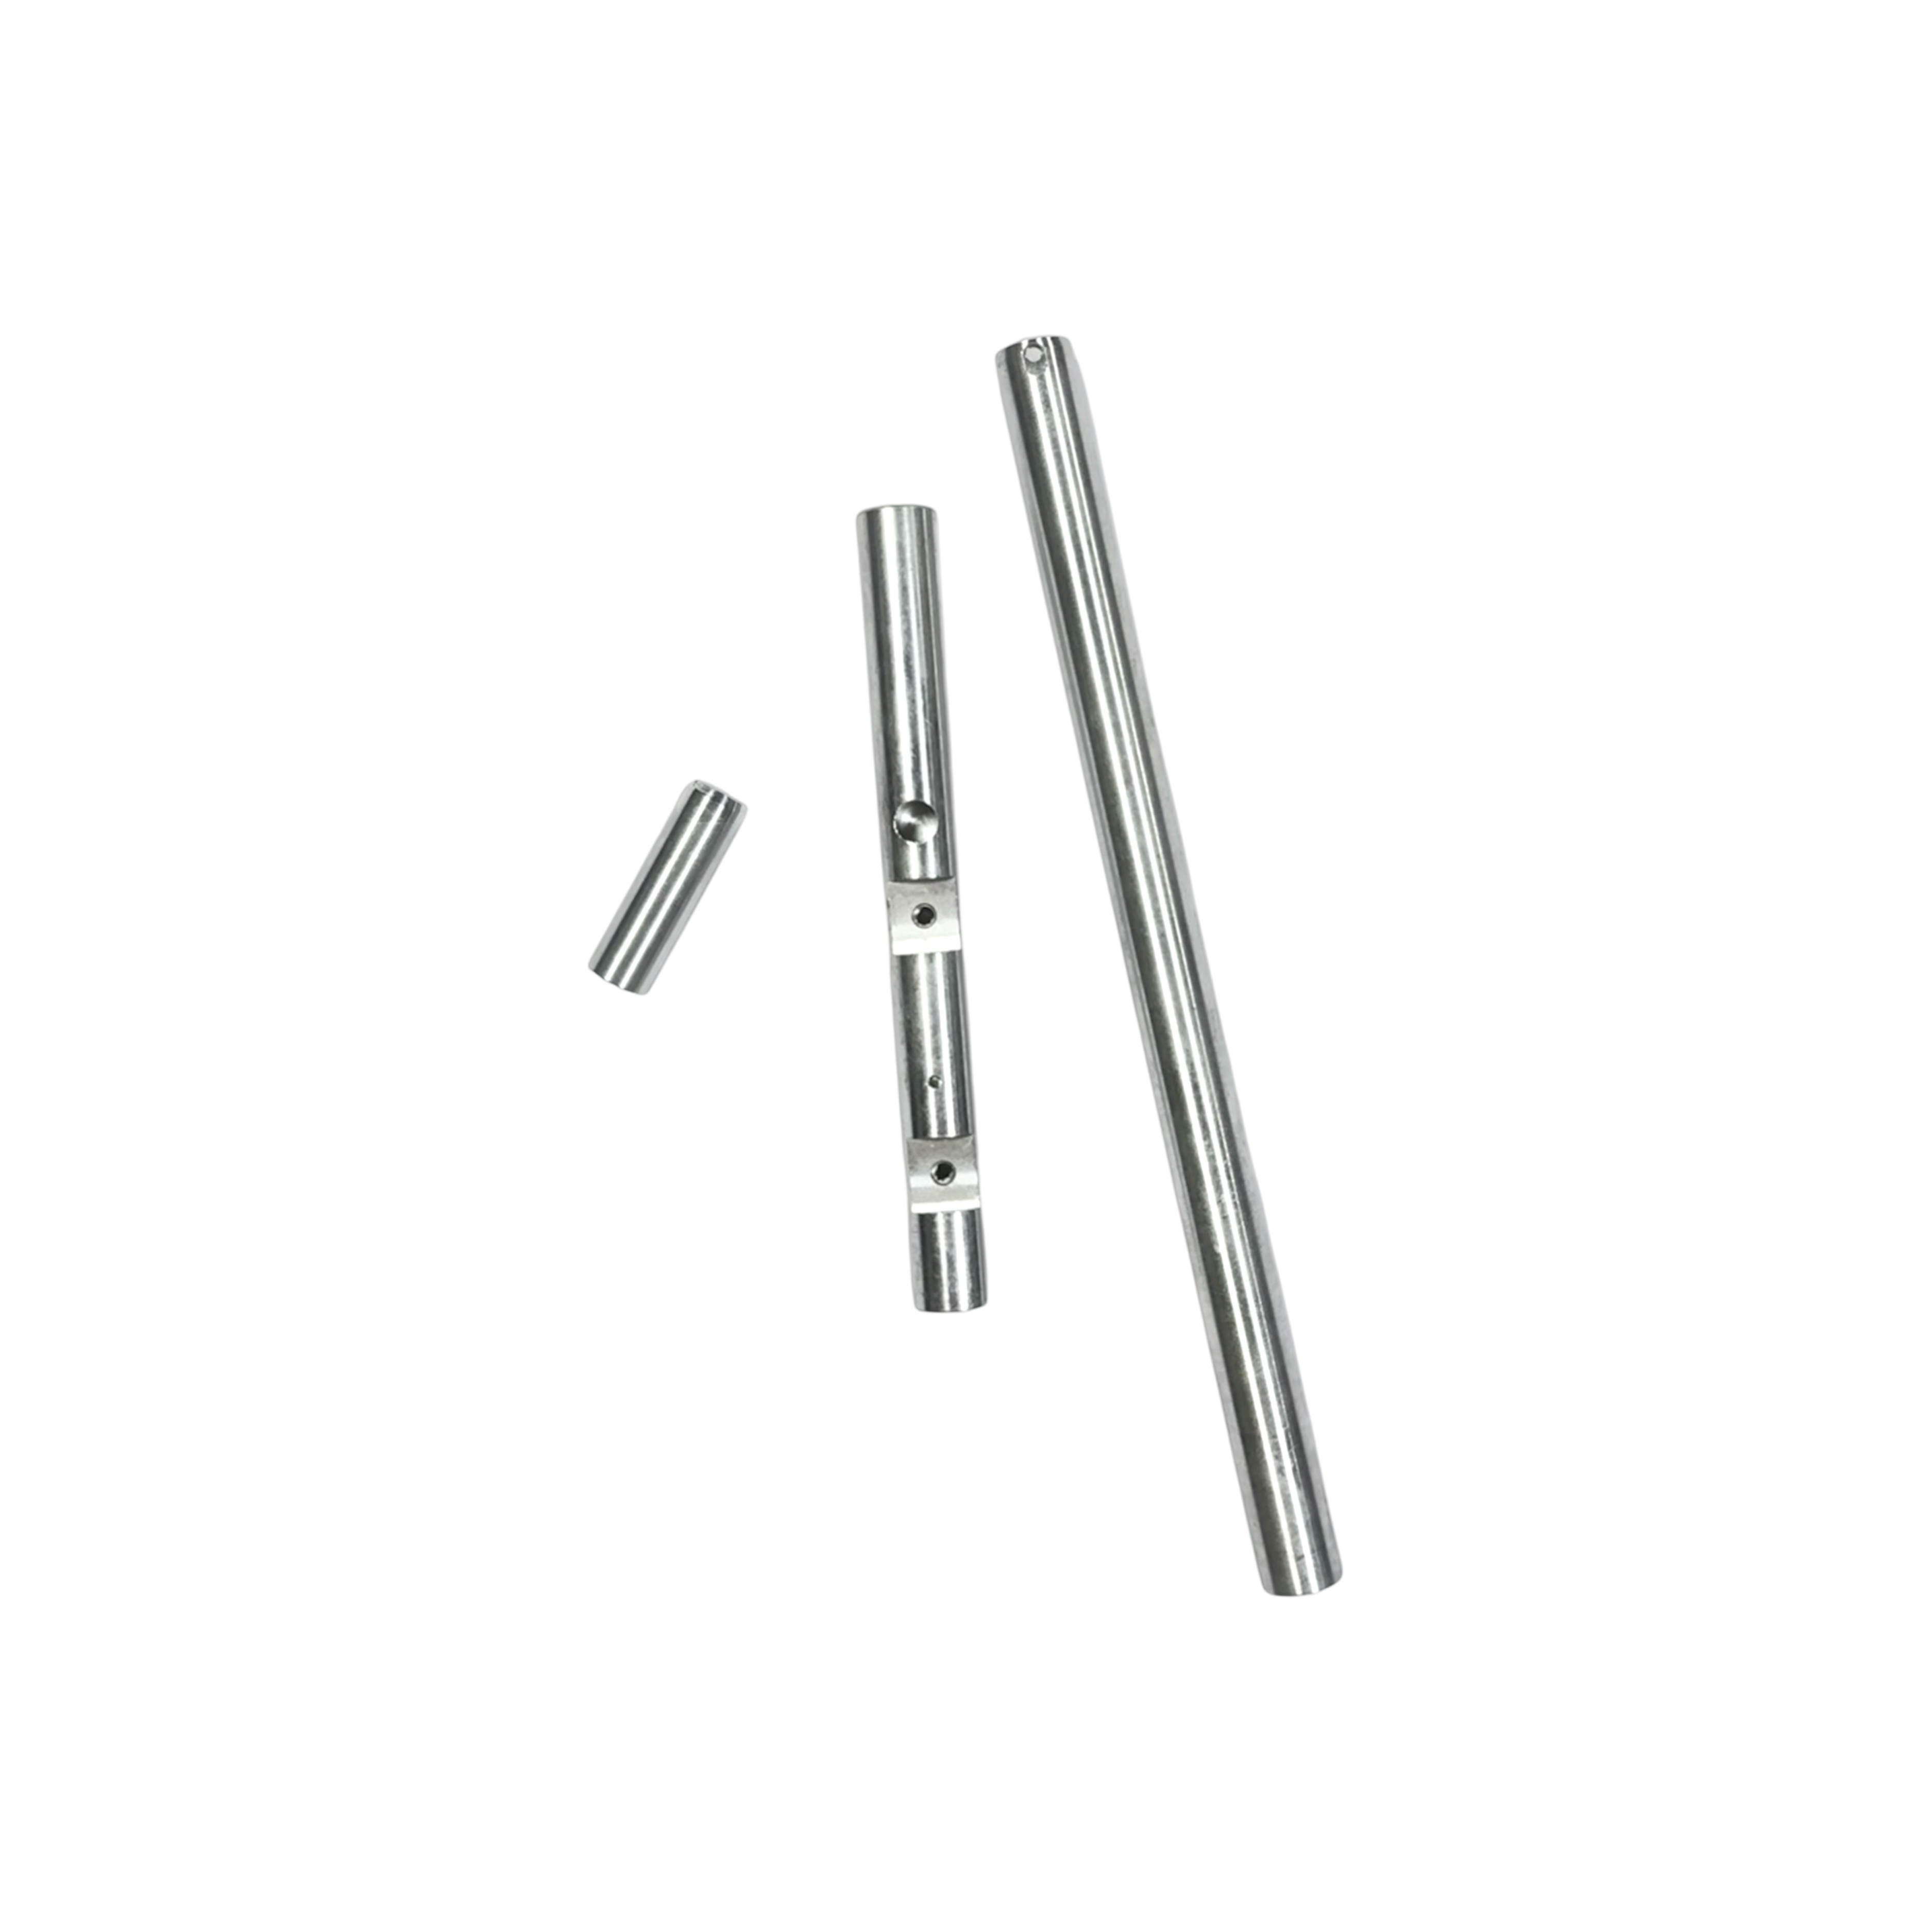
Pins and shaftsSimple or stepped profiles with repeat dimensions.
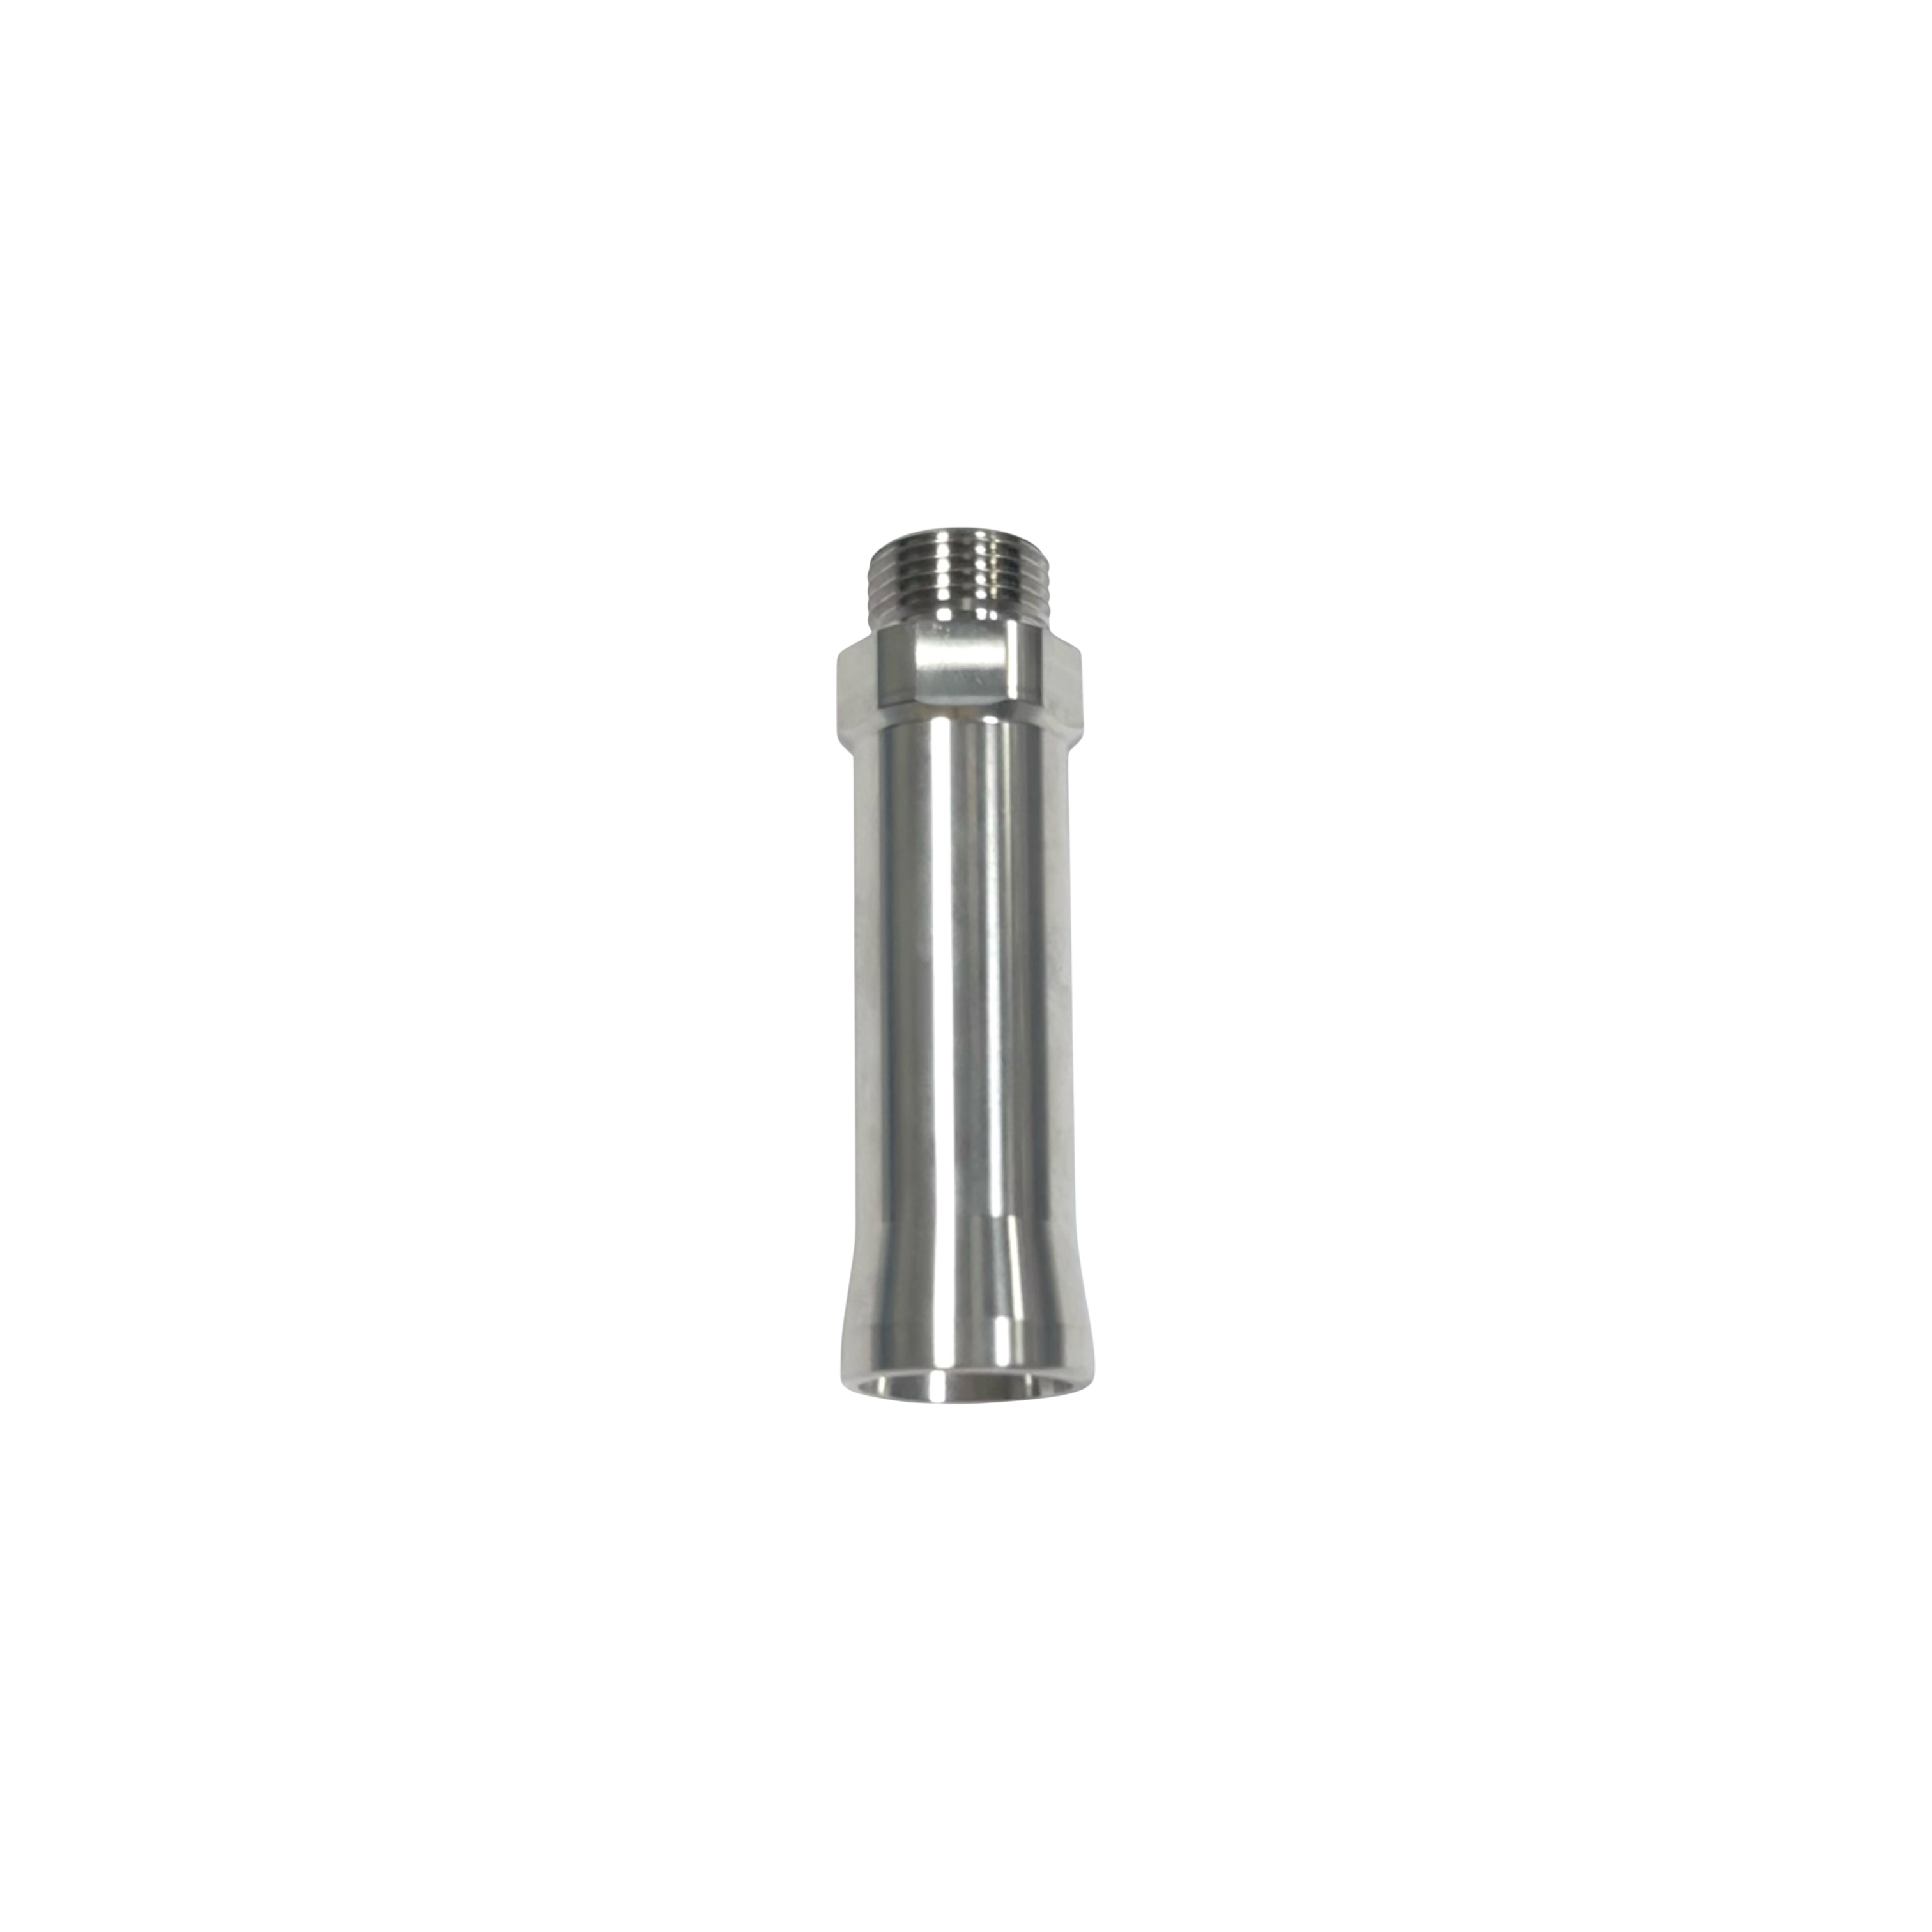
Bushings and sleevesOD/ID relationships, chamfers and controlled edge condition.
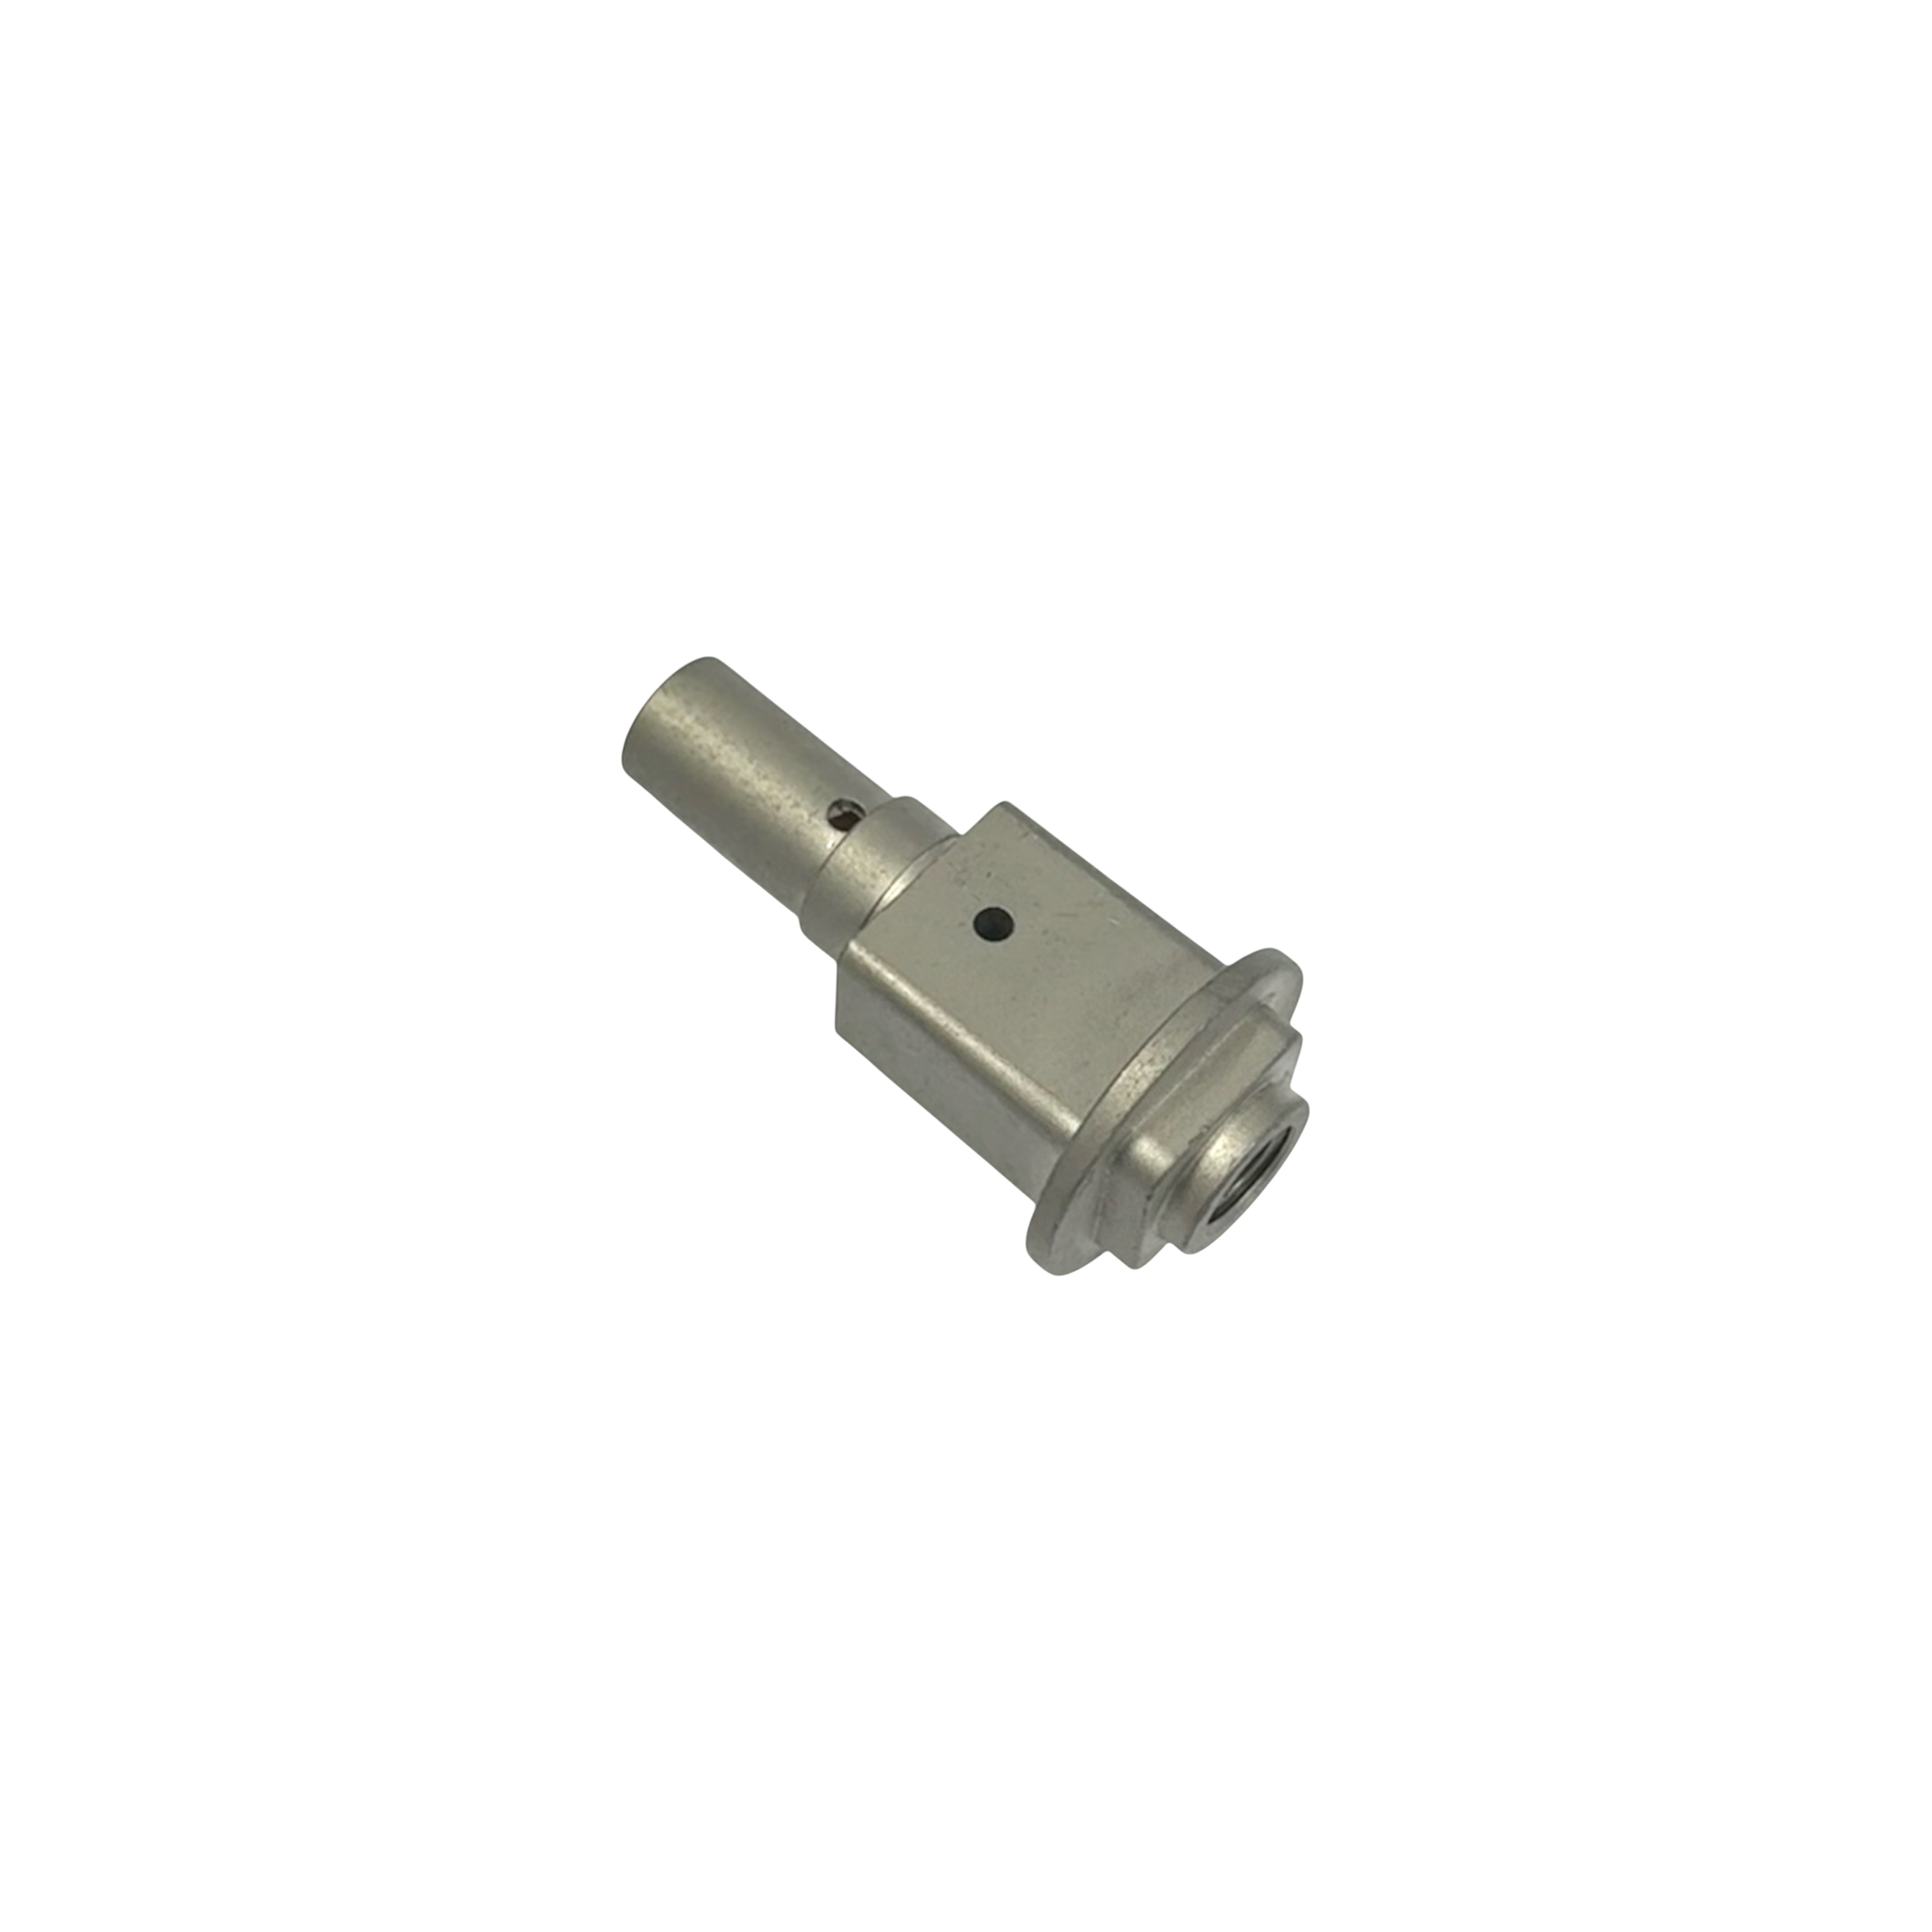
Threaded fittingsRepeat threads, shoulders, seats and wrench features.
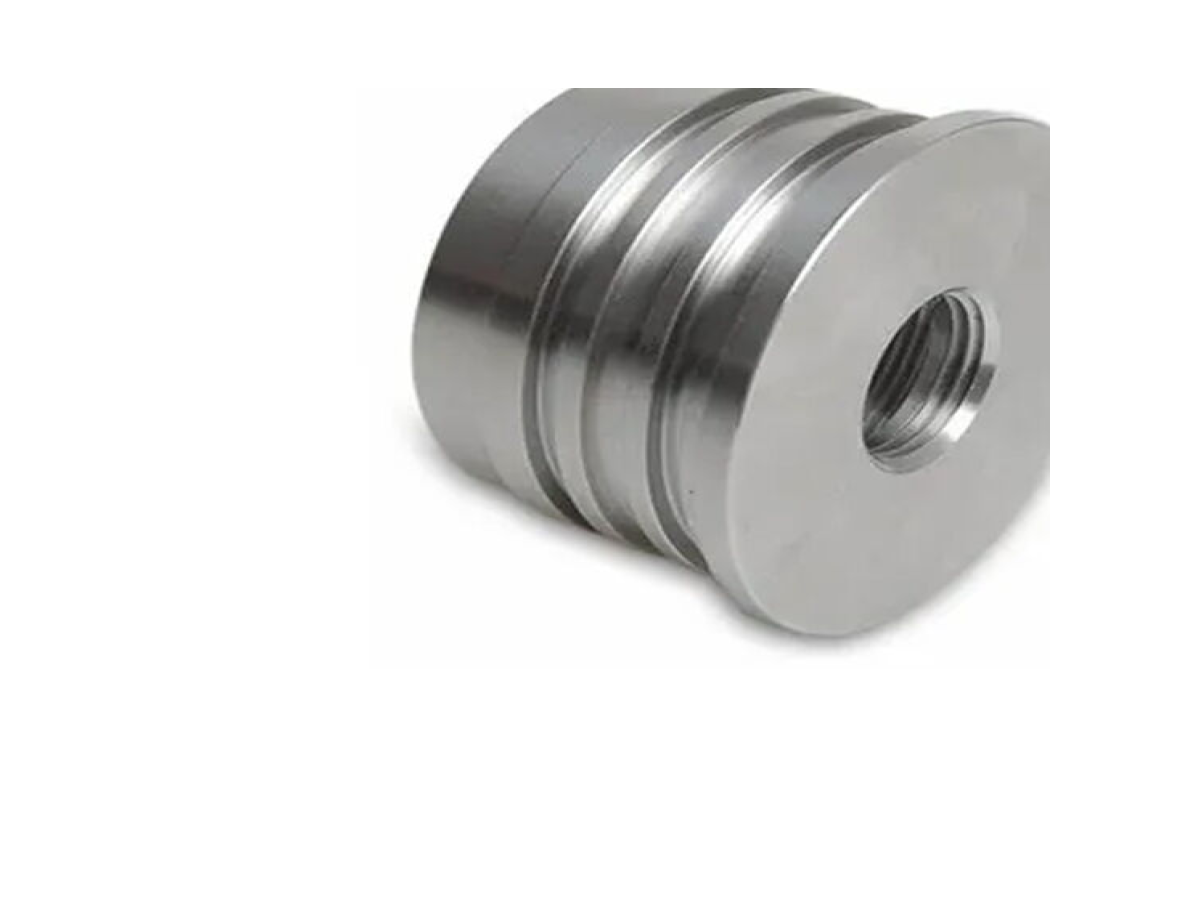
Small collarsStable short components where bar-fed production may fit.
Repeat turned blanksBar-fed repeat parts where quantity and geometry support the route.
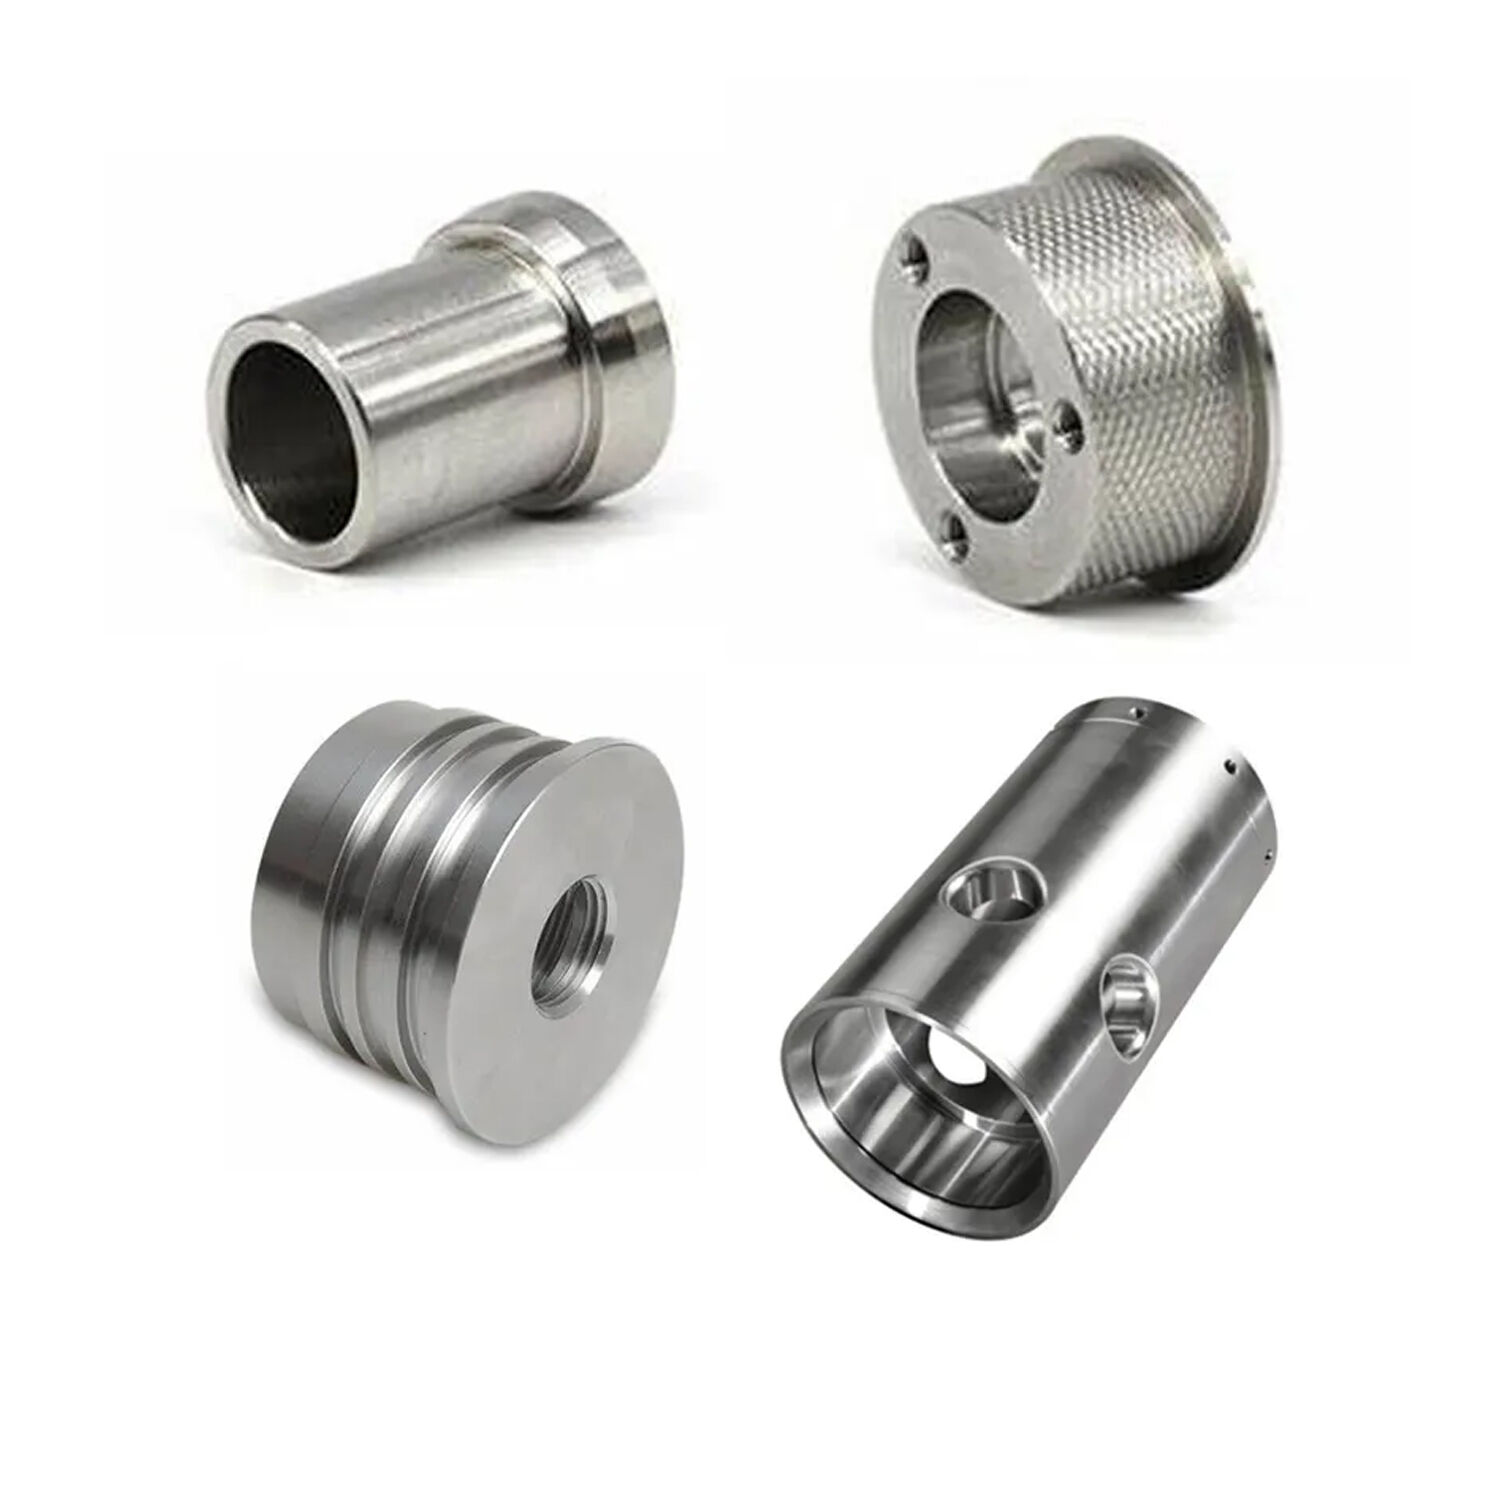
Compact production partsSmall collars, sleeves and machined blanks prepared for repeat orders.
/ Geometry Stability
The 500th part matters as much as the first
Repeat production depends on controlling the features most likely to drift during a run.
Threads, grooves and shoulders can change as tooling wears.
Raw stock diameter and straightness can affect consistency.
Cutoff burr and end-face condition should be specified.
Critical features need planned checks during production.
/ Bar Stock
Input material affects output consistency
For bar-fed work, raw stock quality is part of the manufacturing plan.
Production checkpoint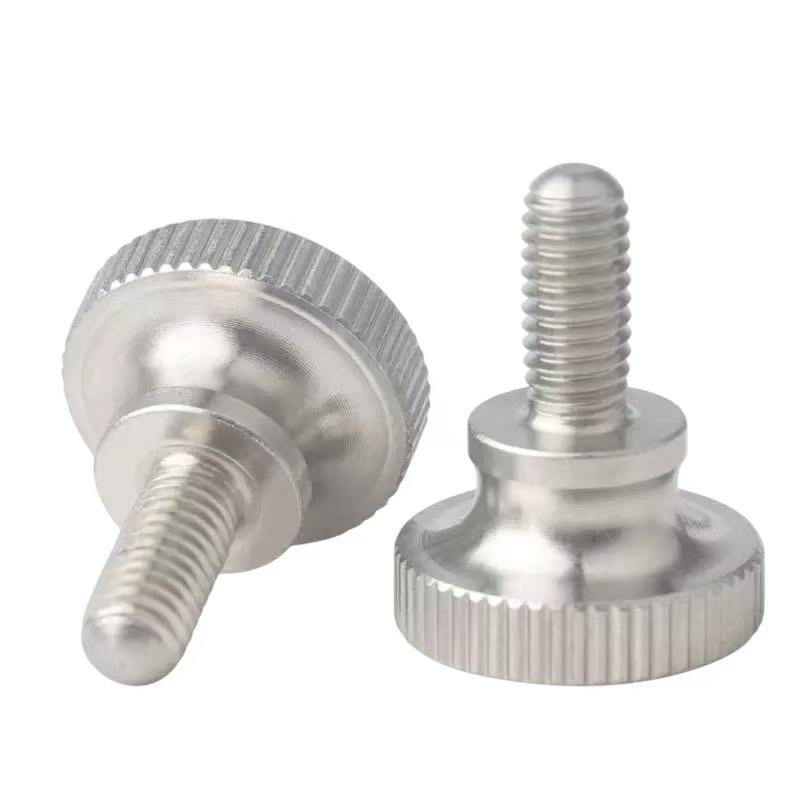
01 / FOCUSBar diameter
Check stock diameter, straightness, grade and surface condition against the production route.
/ Setup and Changeover
Production efficiency starts before the run
Shorter cycle time is useful only when setup, tooling and inspection are stable.
First-piece inspection should confirm the setup.
Repeat parts need predictable tool replacement and offset control.
Frequent design changes reduce the advantage of automatic routing.
Small parts may need handling and cleanliness requirements.
/ Burr and Cleanliness
Fast production still needs a clean part
Burrs, chips and handling marks can reject a dimensionally correct component.
Production checkpoint
01 / FOCUSCutoff burr
Set the acceptable edge and cleanliness condition before the part reaches final inspection.
/ Prototype to Production
Sample first, production route second
A fast prototype route and an efficient repeat route may not be the same. The repeat route should be confirmed before scale-up.
Confirm geometry and function before committing the repeat route.
Check fit, critical dimensions and assembly requirements.
Confirm route stability and inspection checkpoints.
Plan repeat batches when quantity and drawing stability support it.
/ Secondary Needs
Add only the operations the part requires
Automatic lathe output may still need supporting machining, finishing or inspection based on the final drawing.
Production checkpoint01 / FOCUSCross drilling
Define position, size, breakthrough condition and inspection method before machining.
/ Quality Control
Control repeatability through the run
Quality planning should focus on the dimensions and surfaces most likely to affect function.
| Requirement | Manufacturing Focus | Buyer Value |
|---|---|---|
| First-piece approval | Confirm setup before production continues. | Keeps production setup, inspection and final part requirements aligned. |
| In-process checks | Monitor CTQs affected by tool wear or material variation. | Keeps production setup, inspection and final part requirements aligned. |
| Final inspection | Check the completed part and packaging state. | Keeps production setup, inspection and final part requirements aligned. |
| ISO 9001 | Use the quality system as the management baseline, not as a substitute for feature checks. | Keeps production setup, inspection and final part requirements aligned. |
/ PRODUCTION INPUTS
Bring quantity into production planning
Automatic-lathe planning needs production context earlier than one-off machining.
Production checkpoint
01 / FOCUSDrawing
Confirm the part function, material, tolerance and production route before scale-up.
No. Swiss turning is a specific small bar-fed precision route. Automatic lathe is discussed here as a repeat-production route for suitable turned parts.
No. 500+ pcs describes where repeat-production planning often becomes relevant; samples and lower-volume validation can still be reviewed.
Stable turned parts such as pins, sleeves, collars, bushings and threaded fittings are common production candidates.
Send drawings, material, estimated quantity, project stage, critical features, finish requirements and any prior production issues.