/ Material grade
Alloy and carbide structure
Alloy composition and carbide structure influence cutting behavior, tool selection, chip formation and achievable surface condition.
/ High-speed steel & tool steel
Tool steel machining changes significantly with grade, hardness and heat-treatment condition. FREEFLY CNC evaluates these factors together with part geometry and final dimensional requirements to determine a practical machining route.
/ Material families
High-speed steel is different from high-strength structural steel, and individual tool-steel families can behave very differently during machining. Alloy composition, carbide content, hardness and heat-treatment condition influence cutting forces, tool life, surface quality and dimensional stability.
These grades are representative machining examples rather than a material-stock inventory.
/ Material condition
A tool-steel grade in annealed condition can machine very differently from the same grade after pre-hardening or full heat treatment.
As hardness increases, machining may involve higher cutting forces, faster tool wear, greater cutting heat, more demanding surface-finish control, increased sensitivity around small threads and thin features, and different requirements for final machining or grinding.
Material condition therefore influences both the cutting strategy and the sequence used to reach the final dimensions.
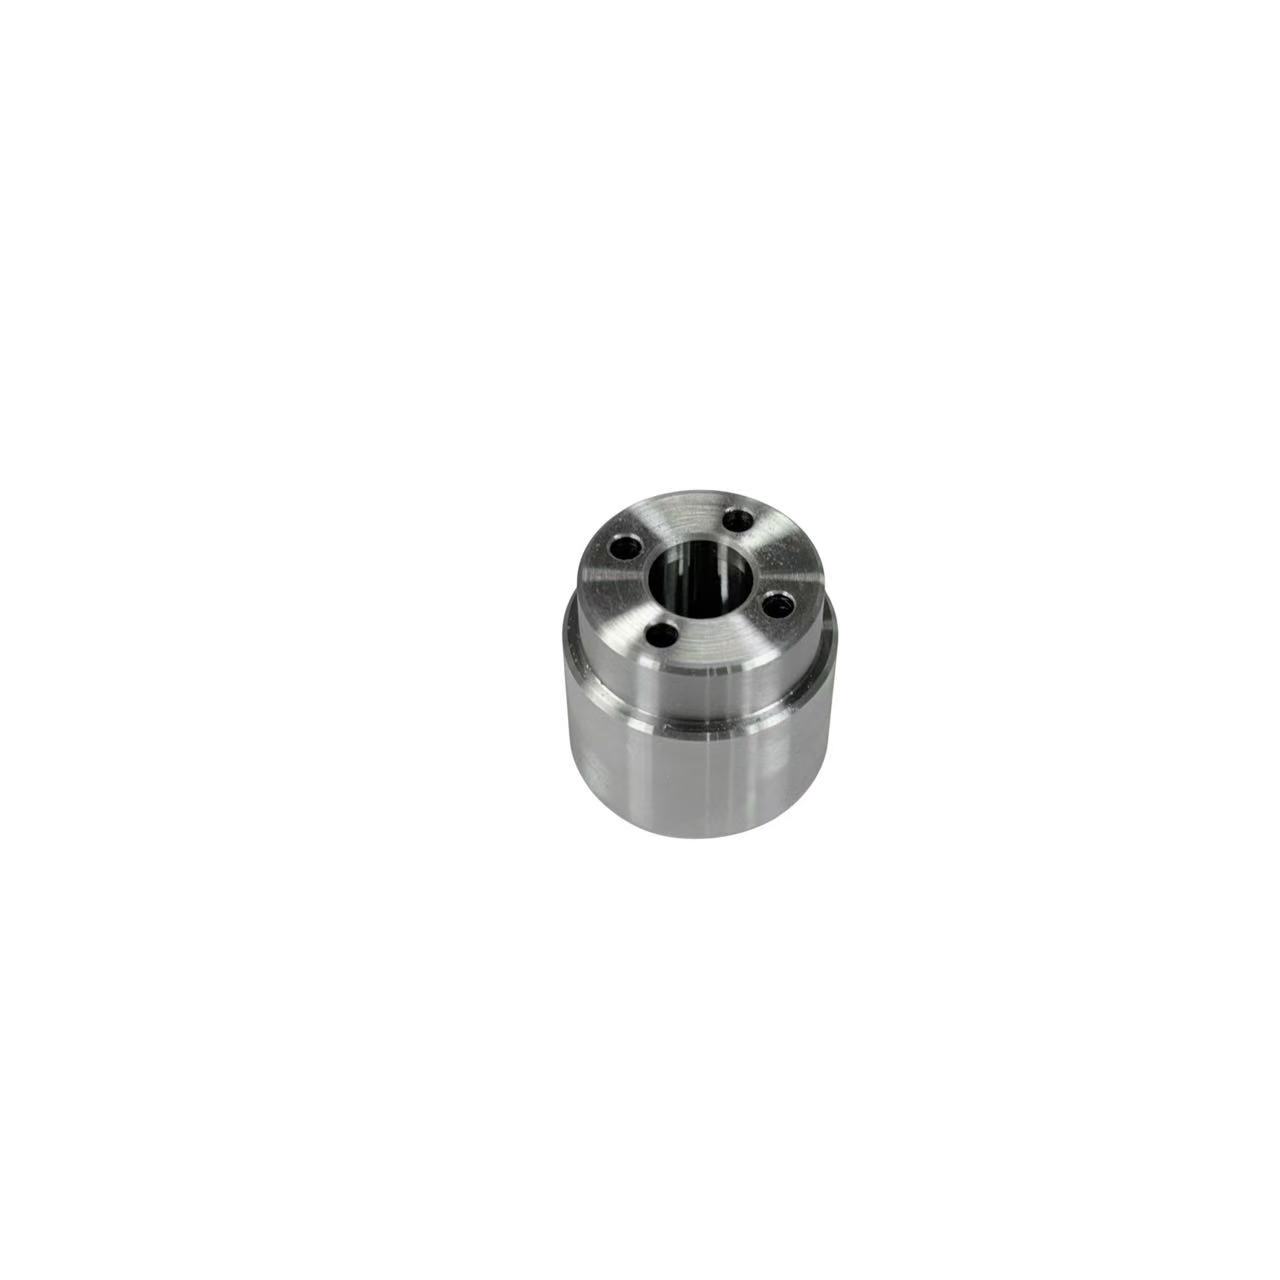
/ Machining behavior
Tool-steel parts are shaped by several interacting factors. Grade alone rarely determines whether a component will machine efficiently.
/ Material grade
Alloy composition and carbide structure influence cutting behavior, tool selection, chip formation and achievable surface condition.
/ Supplied hardness
Annealed, pre-hardened and hardened stock require different cutting parameters and tooling strategies.
/ Final hardness
When heat treatment forms part of the production route, final hardness influences machining allowance and whether precision finishing is required afterward.
/ Part geometry
Thin walls, long shafts, small threads, deep holes and interrupted features can increase cutting-force, chip-control and distortion risk.
/ Final tolerance
Tight dimensional relationships may require different machining stages before and after heat treatment.
/ Production quantity
Longer production runs increase the importance of tool-life control, dimensional monitoring and stable process conditions.
/ Machining challenges
/ Process sequence
There is no single process route for every tool-steel component. A typical sequence may combine soft machining, heat treatment and final finishing according to the grade, geometry and finished-part requirement.
The process begins with the supplied grade and material condition.
Primary geometry is produced while leaving suitable material where later finishing or distortion correction may be required.
Where required by the component, thermal processing establishes the target material condition before final dimensional work.
Critical geometry can be brought closer to final size after the main material and stress changes have occurred.
Hardened features may require controlled machining or coordinated finishing where final hardness and tolerance demand it.
Critical dimensions, surfaces and functional relationships are verified after the required manufacturing sequence is complete.
/ Dimensional stability
A component that is dimensionally correct before heat treatment may not remain unchanged afterward.
For parts with critical post-treatment dimensions, the manufacturing sequence may leave selected features for final machining or finishing after heat treatment.
/ Material characteristics
Tool-steel selection is typically driven by the mechanical requirement of the finished component, while machinability is shaped by the chosen grade and final material condition.
Final material selection remains an engineering decision based on the component's functional requirements.
/ Machining cost
Feasibility depends on the specific grade, hardness, geometry, feature size and final tolerance. Some hardened features can be machined directly, while others may require a different finishing sequence or coordinated downstream process.
Both approaches are used. Many components are rough machined in a softer condition, heat treated, and then brought to final dimensions afterward. The appropriate sequence depends on geometry, hardness and final tolerance.
Hardness directly influences cutting forces, tool wear, heat generation and achievable surface condition. Two pieces of the same grade can require very different machining strategies when their material conditions are different.
Yes. Heat treatment can change straightness, roundness, bore size and other dimensional relationships, particularly on long, thin or asymmetrical parts.
These and related high-speed/tool-steel grades can be evaluated by project. Machining feasibility depends on the actual grade, supplied condition, hardness, geometry and finished-part requirements.